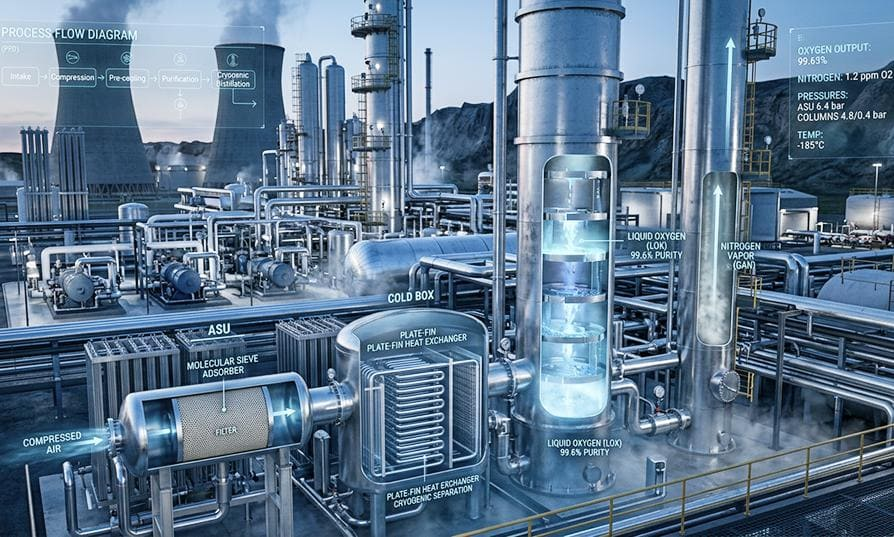
A process-level breakdown of cryogenic air separation — and how every stage of the Oxygen Gas Plant Process directly determines the purity, cost, and reliability of your industrial gas supply.
Sanghi Overseas Team · Oxygen And Nitrogen Plant Manufacturer · Oxygen Plant Supplier In India · 12 min read
Most industrial buyers select an oxygen or nitrogen gas plant based on two numbers: capacity and price. These are necessary inputs, but they are not the whole picture. The process by which oxygen is generated — the sequence of compression, purification, heat exchange, cryogenic separation, and delivery — is what ultimately determines whether your plant runs efficiently, produces gas at the purity your process demands, and does so reliably over a 20-year operating life.
At Sanghi Overseas, an associate concern of Sanghi Organization and a recognised Oxygen And Nitrogen Plant Manufacturer with 1,100+ installations across 90+ countries, we design every plant around the integrity of the Oxygen Gas Plant Process itself. This blog unpacks each stage of that process, explains what can go wrong when plant design shortcuts are taken, and connects process quality directly to industrial efficiency and output quality.
WHY PROCESS MATTERS
The Oxygen Gas Plant Process is not a commodity. Two plants with identical rated capacities can deliver radically different real-world performance depending on whether the compression, molecular sieve drying, heat exchange, and distillation stages have been engineered correctly. At Sanghi Overseas, our medium-pressure cryogenic design — operating at just 32–35 kg/cm² — reflects decisions made at every stage of the process to reduce energy, improve purity, and extend service intervals.
The Oxygen Gas Plant Process — Stage by Stage
Cryogenic air separation is the gold standard for industrial-scale oxygen and nitrogen production. It separates atmospheric air into its components by exploiting the difference in boiling points between oxygen (−183°C) and nitrogen (−196°C). Every stage in the process chain is interdependent — a compromise at one stage propagates inefficiency through all the ones that follow.
1. Air Intake & Compression
Atmospheric air is drawn in and compressed by a multi-stage reciprocating air compressor. In the Sanghi Overseas plant design, starting compression is 45 kg/cm², reducing to 32–35 kg/cm² during normal continuous operation. This medium-pressure design is a deliberate engineering choice — lower operating pressure means lower energy consumption per m³ of oxygen produced, reduced mechanical wear on compressor components, and a longer maintenance interval. A specially designed Cascade Cooler eliminates the need for a separate chilling unit, removing a recurring cost and failure point.
2. Molecular Sieve Pre-Purification
Compressed air passes through a Molecular Sieve Battery Dryer — one of the most important stages in the entire Oxygen Gas Plant Process. This unit simultaneously removes moisture, carbon dioxide, acetylene, and other hydrocarbons from the process air. Removing these contaminants before the air enters the cold box is critical: any water or CO₂ that reaches cryogenic temperatures will freeze and block the heat exchanger passages, degrading efficiency and forcing premature defrost cycles. The Sanghi design eliminates the need for separate acetylene absorbers and removes recurring caustic soda costs — a direct saving in operating cost over the plant's life.
3. Heat Exchange & Pre-Cooling
Purified air enters a highly efficient multi-pass heat exchanger where it is progressively cooled against returning product streams (oxygen, nitrogen, and waste gas). The quality of the heat exchanger design directly determines how much refrigeration energy is recovered from these outgoing streams — and therefore how much additional mechanical refrigeration the expansion engine must provide. Sanghi Overseas plants use a specially designed heat exchanger for maximum cold energy recovery, which reduces the work demanded of the expansion engine and lowers the steady-state power consumption of the plant.
4. Cryogenic Expansion & Refrigeration Generation
A portion of the pre-cooled air is routed through a Hydraulic Expansion Engine — a key component that distinguishes a well-engineered plant from a basic one. The expansion engine does two things simultaneously: it drops the temperature of the air to cryogenic levels by isentropic expansion, and it recovers mechanical energy from that expansion which can be fed back into the system. The Sanghi super-efficient expansion engine achieves rapid initial cooldown (reducing startup time after defrost to approximately 8 hours across most models), maintains the required low temperature during operation, and contributes directly to long-term power savings.
5. Cryogenic Distillation (Air Separation)
Liquefied air enters the distillation column system, where oxygen and nitrogen are separated based on their different boiling points. The lower column operates at higher pressure and produces a nitrogen-rich vapour and an oxygen-enriched liquid. The upper column, operating at near-atmospheric pressure, completes the separation — producing gaseous nitrogen at the top and liquid oxygen at the bottom. The purity of the final products is a direct function of the distillation column design, the reflux ratio, and the quality of the pre-purification upstream. Sanghi Overseas plants consistently deliver oxygen at 99.6% purity and nitrogen at up to 99.9999% (1 PPM) purity — both from the same distillation cycle.
6. Product Compression & Cylinder Filling
Gaseous oxygen produced in the distillation column exits at low pressure (0.1 kg/cm²). For cylinder filling, it must be compressed to 150 kg/cm². Sanghi Overseas plants include an internal compression Liquid Oxygen Pump — a built-in liquid oxygen pump with an internal gas vaporiser — which fills cylinders with bone-dry, high-purity oxygen at the required pressure. The pump operates based on the liquid level in the condenser, handling available quantity continuously without speed adjustments. This design is simpler, more reliable, and produces drier gas than external booster compressor arrangements.
7. Waste Cold Energy Recovery
Nitrogen and waste gas streams returning from the distillation columns pass back through the main heat exchanger, pre-cooling the incoming compressed air (as described in Stage 03). This waste cold energy recovery is what makes cryogenic air separation thermodynamically efficient at scale — the outgoing cold streams do the work of cooling the incoming streams, reducing the refrigeration burden on the expansion engine. The completeness of this recovery is a direct measure of heat exchanger design quality, and it is a major reason why the Sanghi Overseas Oxygen Gas Plant Process achieves 1.0 kWh per m³ of oxygen at 250 m³/hr and above.
How Process Quality Translates to Industrial Efficiency
Understanding the Oxygen Gas Plant Process at a technical level matters because every design decision made by the manufacturer shows up — sooner or later — in your energy bill, your maintenance schedule, your output purity, and your production continuity. Here is how the process stages connect to real operational outcomes.
ENERGY EFFICIENCY
The single largest variable in the long-term cost of operating an oxygen plant is power consumption. At 1.0 kWh per m³ of oxygen (for 250 m³/hr capacity and above), Sanghi Overseas plants deliver one of the lowest energy profiles in the industry. This is the direct result of medium-pressure design, an efficient expansion engine, and a high-quality heat exchanger — all working together through the Oxygen Gas Plant Process chain.
OUTPUT PURITY
Purity is determined upstream — in the molecular sieve dryer and the distillation column. A plant that compromises on either stage will fail to consistently meet the 99.6% oxygen or 99.9999% nitrogen specifications that medical, pharmaceutical, electronics, and precision manufacturing processes demand. As a trusted Oxygen Plant Supplier In India, Sanghi Overseas builds purity assurance into the process design, not the quality control document.
PRODUCTION CONTINUITY
Defrost cycles interrupt production. The longer the interval between defrost cycles and the faster the restart, the higher the plant's effective utilisation. Sanghi Overseas plants run on a 9–12 month defrost cycle (versus industry norms that can be shorter) and restart in as little as 1 hour after a short stop. This is a direct result of the molecular sieve dryer removing contaminants that would otherwise accumulate in the cold box and force early defrost.
Plant Performance Specifications — Sanghi-O RG Series
As an established Oxygen And Nitrogen Plant Manufacturer, Sanghi Overseas publishes transparent performance data for the full SANGHI-O RG series. The table below captures the key operational parameters that define real-world efficiency.
| Parameter | Specification |
|---|---|
| Oxygen purity | 99.6% (medical & industrial grade) |
| Nitrogen purity (standard) | 96% to 99.99% (simultaneous production) |
| Nitrogen purity (high) | Up to 99.9999% (1 PPM) — modified plant |
| Energy consumption | 1.0 kWh per m3 O2 (≥250 m3/hr capacity) |
| Operating pressure (normal) | 32–35 kg/cm2 |
| Startup pressure | 45 kg/cm2 |
| Startup time (after defrost) | ~8 hours (all models except ORG 1000: 1 hr) |
| Startup time (short stop) | 1–1.5 hours |
| Defrost cycle interval | 9 months (standard) / 12 months (ORG 1000) |
| Capacity range | 80 m3/hr to 1,000 m3/hr (standard); custom to 1,500+ m3/hr |
| Product delivery pressure | Up to 150 kg/cm2 (gaseous); up to 200 kg/cm2g (liquid pump) |
| Ambient design conditions | 15°C, 760 mmHg, 50% RH, 0.03% CO2 |
Industrial Applications — Where Process Quality Is Non-Negotiable
The link between Oxygen Gas Plant Process quality and output quality is most visible in industries where the gas is used directly in a production process — not as an ancillary utility, but as an active process input. In these sectors, purity variation, pressure inconsistency, or supply interruption directly impacts product quality and production yield.
Steel & Metal Manufacturing
Oxy-fuel cutting, EAF oxygen enrichment, and ladle refining all require consistent oxygen purity and pressure. Variation in either reduces cutting speed, increases oxidation losses, or affects steel chemistry.
Medical & Healthcare
Medical oxygen must meet pharmacopoeia standards (99.6% minimum). Hospitals, oxygen bottling plants, and surgical facilities require zero compromise on purity — a single substandard batch is a patient safety event.
Pharmaceuticals
Oxidation reactions, fermentation processes, and clean-room applications require nitrogen at ultra-high purity (99.99%+). Trace oxygen contamination in a nitrogen-blanketed pharmaceutical batch can compromise the entire production run.
Electronics & Semiconductors
Soldering, reflow ovens, and semiconductor fabrication use high-purity nitrogen to prevent oxidation. Electronics-grade nitrogen at <10 PPM oxygen impurity is standard — achievable only from a well-designed cryogenic plant.
Food Packaging (MAP)
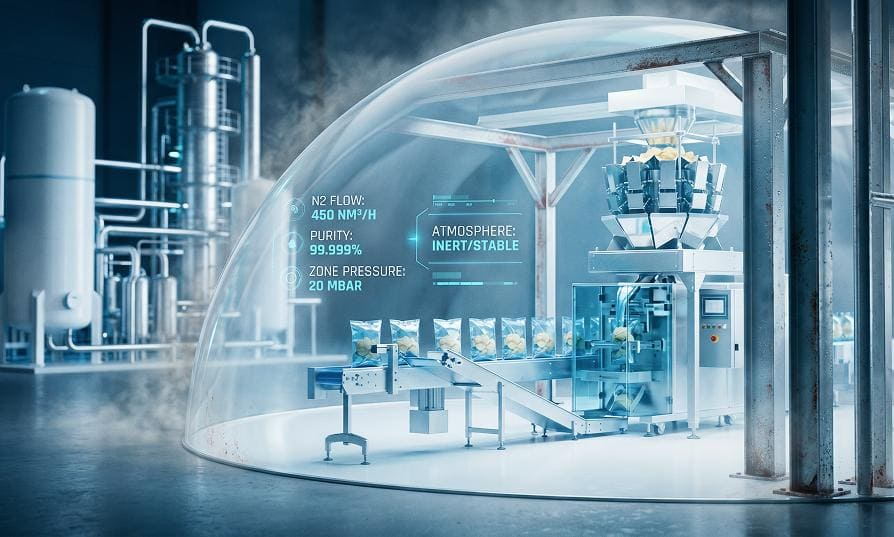
Modified Atmosphere Packaging uses nitrogen to displace oxygen and extend shelf life. The nitrogen purity level directly determines how long the product remains protected — inconsistent purity means inconsistent shelf life, which is a commercial liability.
Glass & Ceramics Manufacturing
Oxygen enrichment of combustion processes in glass melting improves thermal efficiency and reduces NOx emissions. Consistent oxygen concentration is required to maintain melt temperature uniformity and glass quality.
Why the Oxygen Gas Plant Process Design Determines Long-Term ROI
When evaluating proposals from any Oxygen Plant Supplier In India, buyers naturally focus on upfront capital cost. But the Oxygen Gas Plant Process design — which determines energy consumption, maintenance frequency, and output reliability — drives the total cost of ownership over 15–20 years far more than the purchase price alone.
DESIGN TRACEABILITY
Every Sanghi Overseas plant is designed with component traceability and full operator documentation. Our user-friendly, exhaustive operation manual covers every aspect of the Oxygen Gas Plant Process — ensuring your operators understand what each stage does, why it matters, and what to monitor. Plants also provide easy access for maintenance, with design features that minimise downtime during routine service.
Choosing the Right Oxygen And Nitrogen Plant Manufacturer
The Oxygen Gas Plant Process is only as good as the engineering decisions made at the design stage. Sanghi Overseas — operating as both Oxygen And Nitrogen Plant Manufacturer and Oxygen Plant Supplier In India — brings several decades of manufacturing experience, an in-house R&D function, and a track record of 1,100+ installations to every project.
MANUFACTURING DEPTH
Our Taloja, Mumbai manufacturing complex is equipped with the latest engineering equipment for gas plant production. Every plant component is designed by experienced engineers, manufactured from premium materials, carefully inspected before assembly, and run continuously after assembly to verify performance before dispatch. ISO 9001:2015 certification reflects the quality discipline applied across every stage of our manufacturing process.
GLOBAL INSTALLATION BASE
With 1,100+ installations across 90+ countries — including hospitals, steel plants, pharmaceutical manufacturers, and industrial gas distributors — the Sanghi Overseas Oxygen Gas Plant Process design has been validated in the most demanding real-world operating environments. As a Oxygen Plant Supplier In India with extensive export experience, we are equally equipped to support domestic and international buyers through the full project lifecycle.
END-TO-END PROJECT SUPPORT
Sanghi Overseas guides buyers from feasibility study through to post-commissioning lifecycle support. This includes: demand assessment and competitor mapping; technology and capacity selection (cryogenic ASU systems from 50 to 1,500+ m³/hr); infrastructure and site development planning; full equipment supply including air compressors, ASUs, expansion engines, liquid pumps, and storage tanks; and operator training with routine service and spares inventory planning.
Frequently Asked Questions
Everything buyers ask Sanghi Overseas — Oxygen And Nitrogen Plant Manufacturer and Oxygen Plant Supplier In India — about the Oxygen Gas Plant Process and its impact on industrial operations.