Carbon dioxide has quietly become one of the most in-demand industrial gases of the last decade. It carbonates the drinks on supermarket shelves, freezes food during transport, suppresses fires in server rooms, and enriches greenhouse air to grow crops faster. Behind all of it sits a piece of equipment most consumers never think about: the CO₂ recovery plant. As demand for reliable, high-purity CO₂ keeps climbing across food and beverage, industrial, and agricultural sectors, manufacturers are increasingly turning to an established CO₂ plant manufacturer to secure their own supply rather than depend on the open market.
Sanghi Overseas has spent decades engineering CO₂ recovery systems built on modern absorption, purification, and compression technology. This article looks at why CO₂ recovery plants have become essential to modern manufacturing, how they work, and what to look for when choosing a partner to build one.
Why CO₂ Recovery Has Become a Manufacturing Priority
For most of industrial history, CO₂ was treated as a waste product — a combustion byproduct vented into the atmosphere without a second thought. That has changed sharply in recent years. Global CO₂ shortages, driven by fluctuations in ammonia production (a major source of by-product CO₂) and rising demand from food, beverage, and industrial users, have exposed how fragile the open-market CO₂ supply chain really is. Beverage bottlers have had to pause carbonation lines. Meat processors have faced disruptions to stunning and packaging operations. Even hospitals and dry ice producers have felt the squeeze.
This vulnerability has pushed manufacturers to recover and purify their own CO₂ on-site rather than compete for a shrinking, price-volatile external supply. A CO₂ processing plant captures CO₂ that would otherwise be released as flue gas, purifies it to food-grade or industrial-grade standards, and stores it for direct use — turning a waste stream into a dependable, cost-controlled input. This shift is precisely why the search for a proven CO₂ plant manufacturer has accelerated across breweries, bottling plants, food processors, and chemical manufacturers over the past several years.
How a CO₂ Recovery Plant Works
A modern CO₂ recovery plant begins with the controlled purification of CO₂ from combustion or fermentation gases. Flue gases first pass through a pre-cleaning stage to strip out particulates and unwanted compounds, before contacting an aqueous MEA (Monoethanolamine) solution. This absorption method is the industry-proven way to capture CO₂ efficiently while isolating impurities that would otherwise contaminate the final product.
The MEA solution is then heated to release the purified CO₂, which is compressed using specialized compressors. From there, the gas passes through multiple cleaning, drying, and polishing stages to reach food-grade or industrial-grade purity. This multi-step workflow is what allows a well-engineered CO₂ processing plant to maintain consistent output around the clock, rather than fluctuating with feedstock quality or external market conditions.
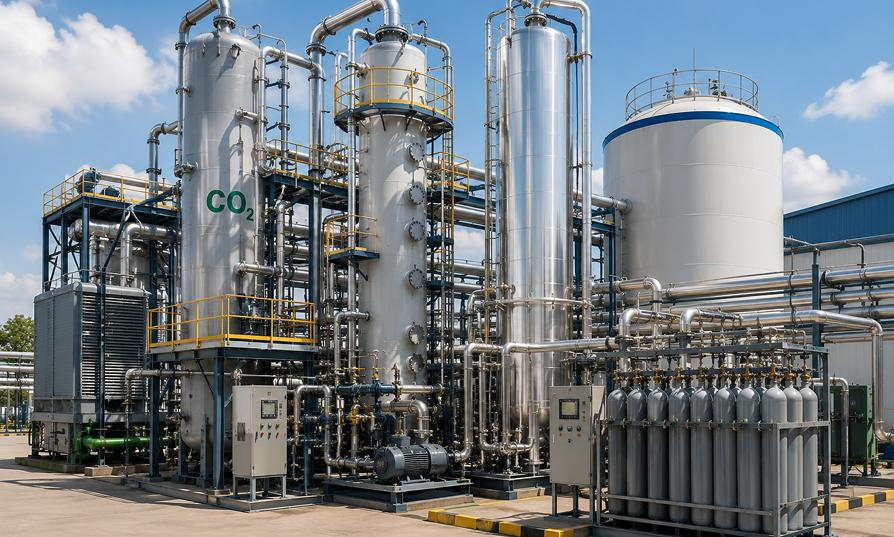
Standard systems typically include combustion and desorption units, absorption and wash columns, compressor stations, cleaning and drying modules, and refrigeration systems for CO₂ liquefaction. Optional additions — storage tanks, CO₂ evaporators, cooling towers, liquid CO₂ pumps, and dry ice machines — let a CO₂ processing plant scale alongside a growing business, which is one of the main reasons modular design has become the industry standard.
Food and Beverage: The Largest Driver of CO₂ Demand
Carbonation is the single largest consumer of purified CO₂ worldwide. Every carbonated soft drink, sparkling water, and draft beer depends on a steady, food-grade CO₂ supply, and any interruption ripples straight through to bottling lines and retail shelves. Because beverage-grade CO₂ must meet strict purity standards — free of odor, taste, and contaminants — bottlers cannot simply source from any available supplier; they need a plant engineered specifically for food-grade output.
This is why beverage manufacturers investing in on-site recovery systems are so selective about their CO₂ plant supplier, checking not just purity specifications but also automation, uptime history, and after-sales support. Dry ice production, another major food-sector application, places similar demands on purity and consistency, since dry ice used in food transport and cold-chain logistics must meet the same food-safety standards as the CO₂ used for carbonation itself.
Industrial and Safety Applications of CO₂
Beyond food and beverage, CO₂ plays a critical role in industrial safety and fabrication. Fire suppression systems in server rooms, electrical installations, and marine vessels rely on CO₂'s ability to displace oxygen and smother flames without leaving residue — making it one of the most trusted agents for protecting sensitive equipment. Welding and metal fabrication industries use CO₂ as a shielding gas, protecting the weld pool from atmospheric contamination during MIG welding processes used across automotive, construction, and heavy manufacturing.
Both applications demand a dependable, high-purity gas stream, which is exactly what a properly engineered CO₂ processing plant is built to deliver. Manufacturers in these sectors increasingly prefer working with a single CO₂ plant manufacturer capable of tailoring output specifications to their exact application, rather than managing multiple external suppliers for gas that ultimately needs to meet the same rigorous standard every time.
CO₂ in Agriculture and Greenhouse Enrichment
One of the fastest-growing applications for recovered CO₂ is greenhouse enrichment. Elevated CO₂ concentrations inside controlled greenhouse environments measurably accelerate photosynthesis, boosting crop yield and shortening growing cycles for high-value produce. As commercial greenhouse operations scale up, particularly in regions investing heavily in controlled-environment agriculture, the demand for a consistent, cost-effective CO₂ supply has grown alongside it.
For large greenhouse operators, sourcing recovered CO₂ from a reliable CO₂ plant supplier is often more economical than purchasing bottled CO₂ at commercial volumes, particularly when the greenhouse operation is co-located near an industrial facility already generating CO₂-rich flue gas as a byproduct.
What to Look for in a CO₂ Plant Manufacturer
Across every application — food and beverage, fire suppression, welding, or agriculture — a few requirements repeat: consistent purity, energy-efficient operation, automated controls that minimize downtime, and durable, low-maintenance construction that keeps the plant running for decades. A plant that cannot hold food-grade purity is unusable for beverage carbonation. A plant with excessive downtime defeats the entire purpose of moving away from external CO₂ dependency.
This is where the choice of CO₂ plant manufacturer becomes a long-term decision rather than a simple procurement exercise. Buyers should evaluate a prospective CO₂ plant supplier on installation history, certifications, technical support during commissioning, and the availability of spares and service well after the initial sale — since a recovery plant is typically expected to run reliably for twenty years or more.
Sanghi Overseas: Turnkey CO₂ Recovery Systems
Sanghi Overseas designs turnkey CO₂ processing plant systems built on proven MEA absorption, multi-stage purification, and compression technology, engineered to deliver high-purity, food-grade CO₂ with minimal maintenance. With a modular layout that includes combustion and desorption units, absorption and wash columns, compressor stations, and refrigeration systems for liquefaction, each plant is designed to scale as a business grows — with optional storage tanks, evaporators, cooling towers, and dry ice machines added as needed.
As an ISO 9001:2015 certified CO₂ plant manufacturer and CO₂ plant supplier with decades of engineering expertise, Sanghi Overseas provides full technical support from design through commissioning, giving food and beverage producers, industrial manufacturers, and agricultural operators a dependable partner for their CO₂ recovery needs.
Looking to set up your own CO₂ recovery or processing plant? Get in touch with Sanghi Overseas' specialists to discuss your capacity, purity, and application requirements